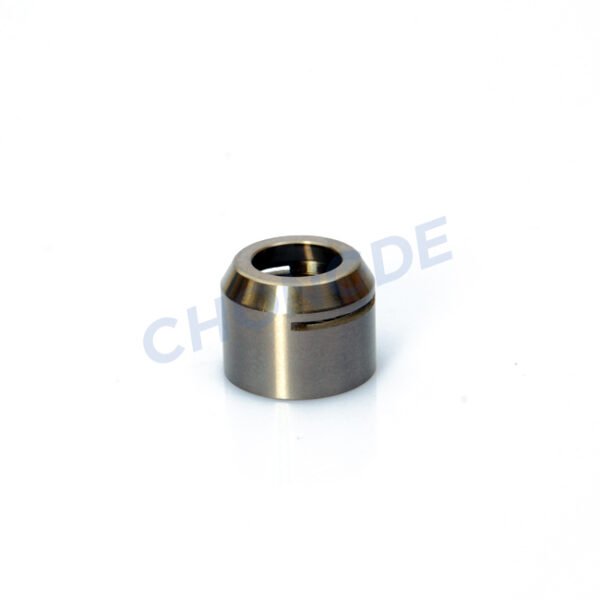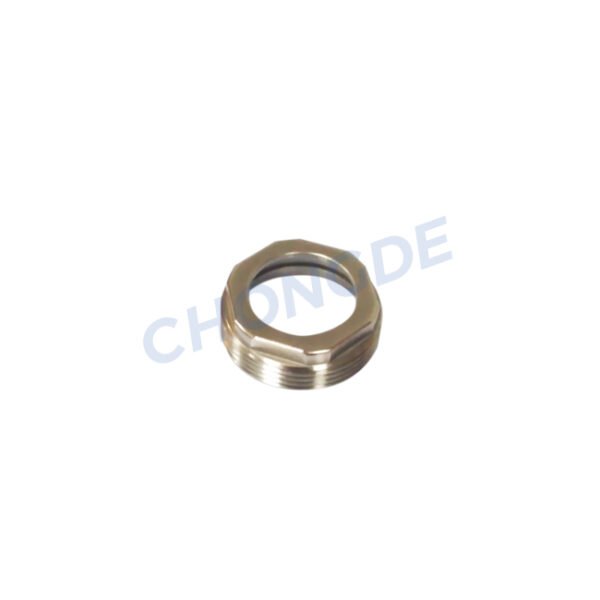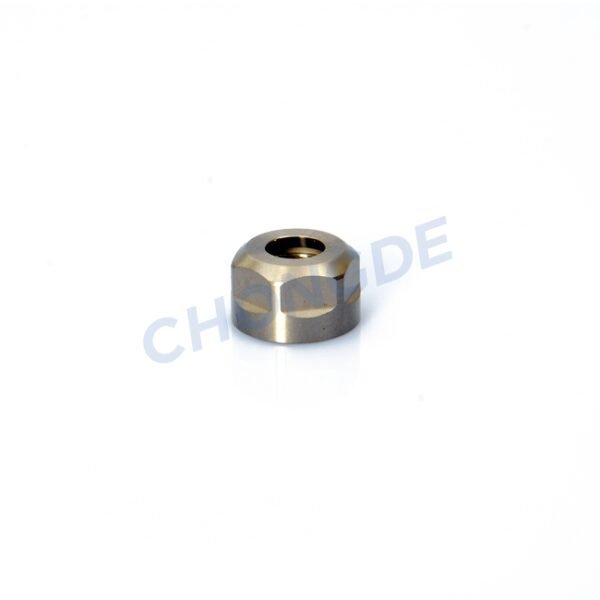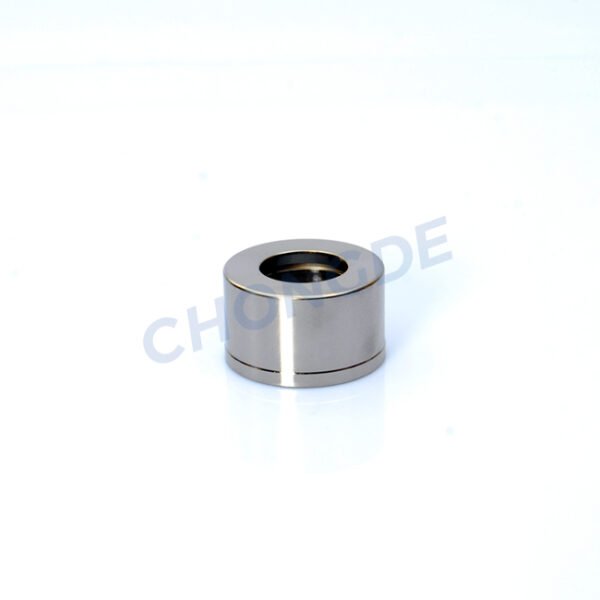
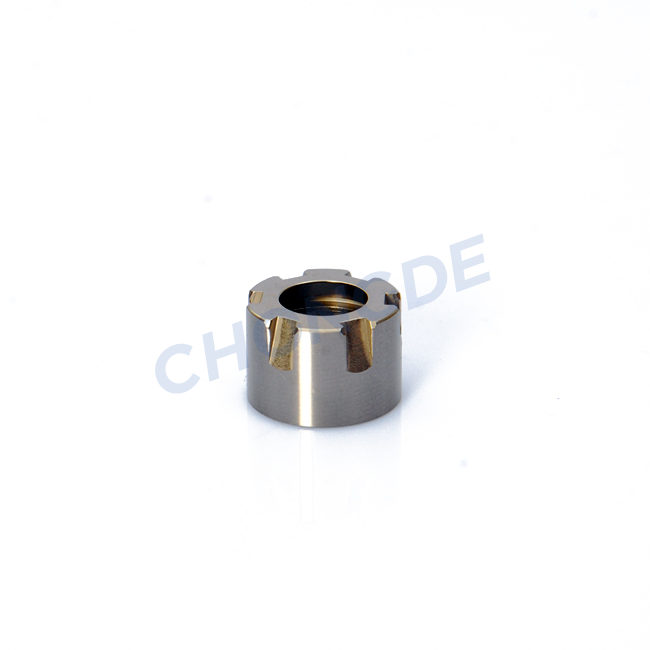
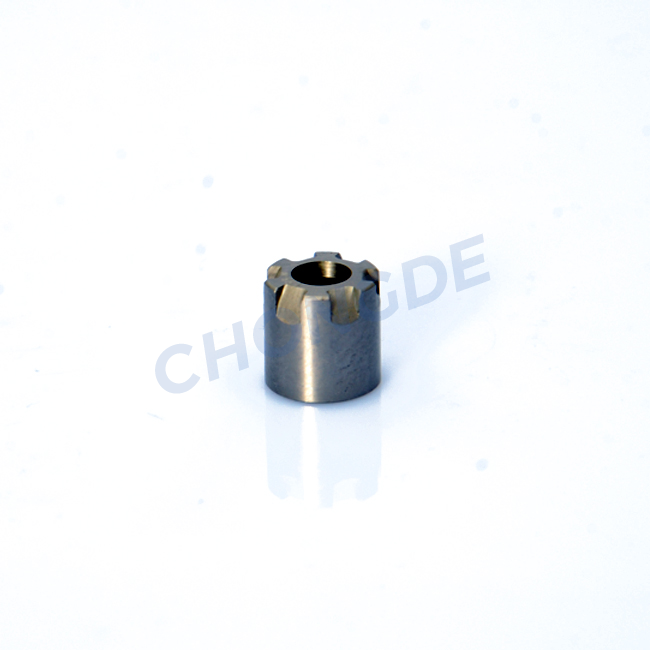
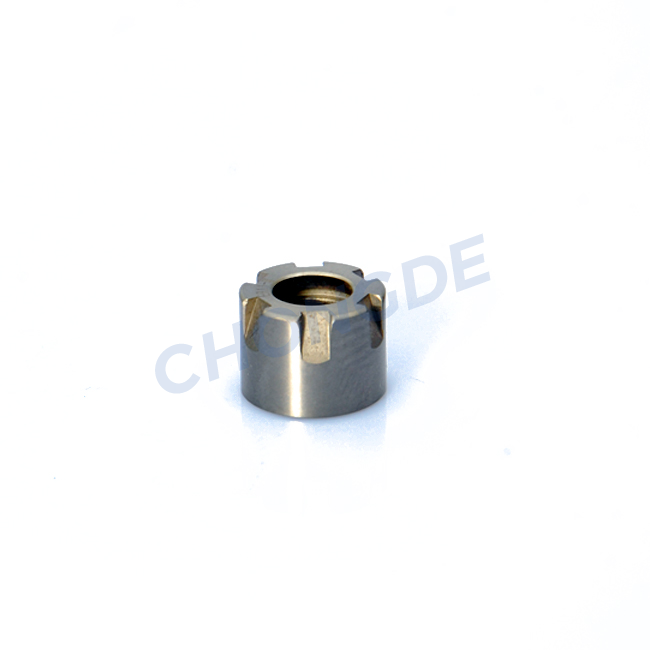
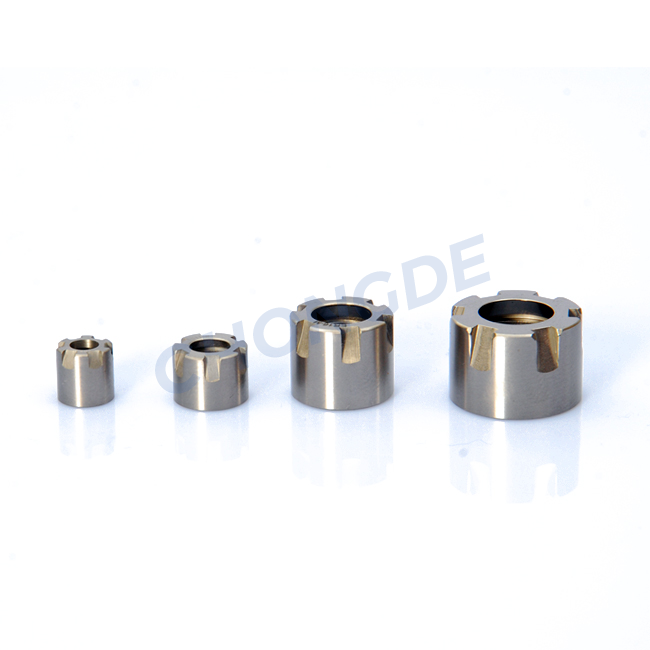
Nickel Coating ER M Type Nut
- Manufactured to DIN / ISO / ANSI standards
- Antirust nickel plating & mirror finish
- OEM / ODM & custom sizes available
- Fast worldwide shipping
Nickel Coating ER M Type Nut
Chongde ER M Type Nut made by 20CrMnTi material. All the nuts are through long time cryogenic treatment and thermal aging treatment to improve the stability of accuracy and dimensions. All the ER nuts are pre balanced G2.5 20000rpm and G2.5 30000rpm. The surface with nickel coating that can improve the hardness and endurance of nuts. Also it has cleaness better, anti-rust, stable accuracy and smooth surface features. ER M type nut using with BT/HSK/CAT/BBT/NT-ER tool holder and ER straight shank collet chuck. The ER M type Nut is used with ER M type wrench.
Features:
1. Material: 20CrMnTi
2. Hardness: 50-53 HRC;
3. Thread Tolerance: 4H;
4. Pre balance is G2.5 20000rpm/30000rpm;
Our advantages
1. Nickel coating surface: antirust, surface smooth and high endurance.
2. 20CrMnTi material: high hardness 50-53 HRC.
3. Default balancing G2.5 20000rpm/30000rpm
4. Cryogenic treatment and thermal aging process. Stable accuracy and long using lif
Product Drawing and Size
| Order No. | Type | Model No | D | L | T |
| CD010307.0812010 | M | ER8M | 12 | 11 | M10x0.75P |
| CD010307.1116013 | ER11M | 16 | 12 | M13x0.75P | |
| CD010307.1622019 | ER16M | 22 | 18 | M19x1.0P | |
| CD010307.2028024 | ER20M | 28 | 19 | M24x1.0P | |
| CD010307.2535030 | ER25M | 35 | 20 | M30x1.0P |
Mounting instruction for ER collets and Nuts
1. Put the collet into the nut,turn the collet slightly. Push it into the nut at the offered direction evenly when the offset flange sinks into the undercut of the collet.
2. Fix the nut and the collet on the spindle rotate the nut until the collet is in pressing, Wipe the straight shank of cutter , and instert it into the pilot hole. Tighten the nut with a wrench till the cutter is clamped heavily (Caution:never tighten the nut without cutter in it for it will break).
3. When changing the tool.Loosen the nut and it shall bring out the collet and the cutter together.And then draw the cutter out push out slightly the collet in the offered direction,it shall be ready for any change of the cutter.
| Order No. | Type | Model No | D | L | T |
| CD010307.0812010 | M | ER8M | 12 | 11 | M10x0.75P |
| CD010307.1116013 | ER11M | 16 | 12 | M13x0.75P | |
| CD010307.1622019 | ER16M | 22 | 18 | M19x1.0P | |
| CD010307.2028024 | ER20M | 28 | 19 | M24x1.0P | |
| CD010307.2535030 | ER25M | 35 | 20 | M30x1.0P |
Send an Inquiry
Fill in the form and our engineers will reply within 24 hours.